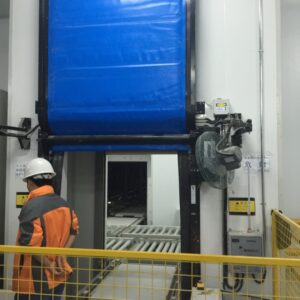
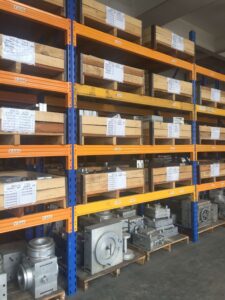
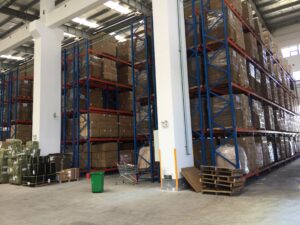
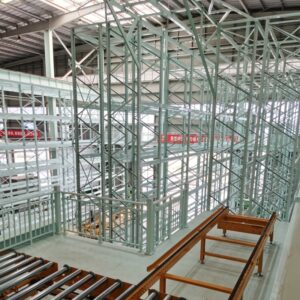
Real-world workshop project launch: The integrated intelligent warehousing system consisting of complete sets of automated AS/RS racking and roller conveyor lines replaces traditional manual warehouses, realizing full-process automatic operations for material storage and handling.
I. Automated AS/RS Racking Efficient space utilization: Modular high-rise steel racks make full use of vertical factory space, tripling storage capacity and greatly cutting floor space occupation. Standardized safe storage: Equipped with safety fencing and structural reinforced components; standardized storage bays stably hold heavy materials to prevent falling and collision damage. Unmanned automatic storage & retrieval: Matched with stacker crane linkage system to fully automate inbound and outbound cargo handling, eliminating forklifts and manual transportation.
II. Fully Automatic Conveyor Lines Intelligent unmanned transportation: Photoelectric sensors installed along the whole line enable automatic start-stop, achieving fully automated material circulation and minimizing manual intervention. Seamless logistics flow: Connects AS/RS racks with production workstations to form a closed-loop logistics channel covering inbound storage, inventory keeping and outbound delivery. Parallel multi-task operation: Multiple parallel conveying channels boost cargo throughput to accommodate high-volume material turnover.
III. Digital Centralized Control System (Attached picture: Industrial control display & operation console) Unified system management of storage bays, inventory and order data; real-time visual warehouse status displayed on large screens. Unique coding for each batch of materials enables full lifecycle traceability, eliminating material confusion, wrong deliveries and inventory discrepancies. One-click remote equipment scheduling to simplify warehouse operation procedures.
Core Project Advantages Cost reduction & efficiency improvement: Over 60% cut in warehouse labor costs with multiplied inbound & outbound efficiency. Less product damage: Mechanized transportation avoids scratches and breakages caused by manual handling. Easy management: Standardized and digital warehouse management with simple maintenance. Strong scalability: Modular equipment supports capacity expansion according to factory production demands
Zhongyue Huateng roller conveyor line, with its precise transmission, modular design and intelligent drive, is suitable for industries such as electronics manufacturing, food and medicine, logistics and warehousing.
Spring’s Arrival Heralds a Golden Era of Growth for ZhongYue HuaTeng As spring quietly unfolds and nature awakens, ZhongYue HuaTeng is entering a golden phase of development. Currently, multiple projects under the company’s umbrella are in ful...
With its innovative design, the Double Deep Racking breaks through the limitations of traditional warehousing, doubles the storage space, and significantly improves the warehouse's volume ratio.
 StorLogi